

Raw Material Mix Ratio for Paver Blocks Produced by Automatic Block Machines
Abstract
The mix ratio for paver blocks produced on automatic block machines differs fundamentally from conventional concrete proportioning. Because these machines rely on zero-slump, semi-dry mixtures that are compacted by vibration and hydraulic pressure and stripped immediately, the acceptable ranges for water content, cement dosage, and aggregate grading are narrower and more interdependent than in cast-in-place concrete. This article synthesizes publicly verifiable data from industrial production records and peer-reviewed studies to establish a practical framework for mix design. It examines the critical relationship between water-cement ratio and machine compaction, the distinct requirements of face-layer versus body-layer mixes in colored pavers, and the adjustments necessitated by supplementary cementitious materials. The analysis concludes that successful mix design for automatic block machines is not a search for an optimal fixed recipe but a calibration exercise bounded by the machine‘s compaction capability, the aggregate’s moisture state, and the target strength grade.
1. Search Intent and User Concerns
Users searching for this topic fall into four intent categories. Technical matching seekers—typically engineers and production supervisors—require a reference proportion range they can adapt to their specific aggregates and machine. Budget optimization seekers, including contractors and distributors, want to reduce cement content without compromising strength or causing rejection rates to rise. Troubleshooting seekers are existing operators whose blocks exhibit low strength, delamination, or mold sticking, and who suspect the mix as the root cause. Application guidance seekers are procurement managers evaluating whether a proposed mix is compatible with a specific automatic machine model before purchase.
The recurring questions are practical: What cement-to-aggregate ratio is appropriate for M30 versus M40 pavers? How does the zero-slump requirement change water control? What pigment dosage is effective in face layers, and at what point does additional pigment cease to improve color? How must proportions shift when fly ash or stone powder replaces a portion of the cement or sand?
2. Quick Answer
For paver blocks on automatic vibro-press machines, published industrial and experimental data converge on a cement content of approximately 350–400 kg/m³ for wear-resistant pavers, with a water-cement ratio in the range of 0.35–0.40 and total moisture (including aggregate surface water) controlled around 6.5–7.0% . A documented production mix from a Brazilian industrial line using an automatic hydraulic vibro-press comprised 160 kg cement, 400 kg sand, 200 kg stone powder, and 200 kg crushed stone per batch, with a water-cement ratio of 0.397 and total moisture capped at 6.5–7.0% . For colored face layers, pigment dosage is typically 3–6% by weight of cement, with saturation generally occurring between 5% and 6% .
3. Key Takeaways
Zero-slump is non-negotiable. Automatic machines strip pallets immediately after compaction; a mix that is too wet will deform or stick to the mold. Total moisture, not just added water, determines success .
.369Cement content for pavers exceeds that for hollow blocks. Wear resistance and surface durability demand a denser binder matrix; published guidance places pavers at 350–400 kg/m³ cement, compared with 250–350 kg/m³ for structural blocks .
Water-cement ratio interacts with compaction energy. A lower W/C ratio yields higher strength only if the machine can achieve sufficient density. Under-compaction negates the benefit of a rich mix.
Pigment saturation limits are real. Beyond approximately 5–6% by cement weight, additional pigment produces minimal color improvement and may increase water demand, affecting face-layer integrity .
Supplementary materials require re-validation, not simple substitution. Fly ash, stone powder, and recycled aggregates alter water demand and early strength development; replacement ratios validated in laboratory studies may not transfer directly to high-speed automatic production.
4. Practical Case: Industrial Production Data
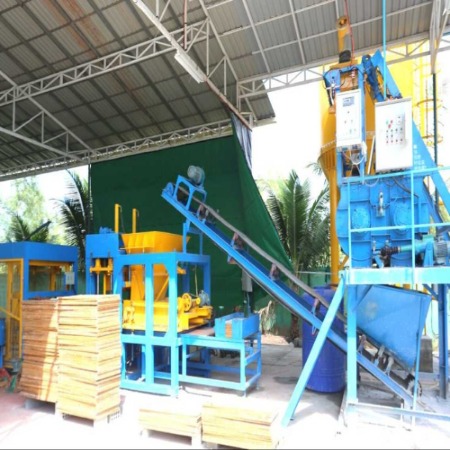
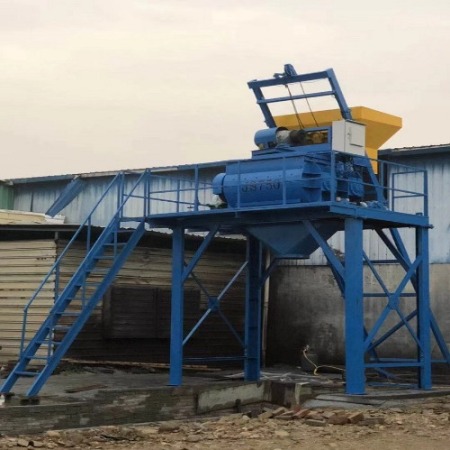
The most directly applicable data point for engineers seeking a reference mix comes from a documented industrial production line using a Trillor MBX-975 Multibloc automatic hydraulic vibro-press. The per-batch mix comprised 400 kg sand, 200 kg stone powder, 200 kg crushed stone, and 160 kg cement, with 59 liters of water and 5 liters of plasticizer solution (approximately 3% of cement mass). The water-cement ratio was 0.397, and total moisture was maintained between 6.5% and 7.0% by internal mixer sensors . This is not a laboratory-optimized mix but a production mix running continuously in a commercial plant, which gives it practical credibility that experimental proportions often lack. Engineers adapting this reference should recognize that the aggregate sources in their region will differ in grading and absorption, and that the machine’s compaction pressure and vibration frequency will influence the acceptable moisture window.
5. FAQ
What water-cement ratio should be used for pavers on an automatic machine?
Published guidance for pavers recommends 0.35–0.40 . An industrial production record documents 0.397 with total moisture at 6.5–7.0% . The lower end of the range is appropriate for high-strength grades and machines capable of high compaction energy; the upper end may be necessary if aggregates are angular and poorly graded.
How much cement is needed for M30 versus M40 pavers?
Mix design references place paver cement content at 350–400 kg/m³, with M30 mixes at the lower end and higher-strength or wear-critical applications toward the upper end . The difference between grades is typically achieved through a combination of cement content and W/C ratio reduction, not cement content alone.
What pigment dosage is effective for colored face layers?
For gray cement, 3–6% by weight of cement is the recommended range; saturation occurs at 5–6% . White cement requires lower dosages, typically 1–4%, to achieve pastel shades. A low W/C ratio in the face mix enhances color intensity at a given dosage.
Can fly ash replace cement in machine-produced pavers?
Yes, but with caution. Experimental studies report fly ash replacement up to 25–30% with acceptable 28-day strength, but early strength development is slower . Automatic machines require sufficient early strength for immediate stripping and stacking; replacement levels that work in laboratory casting may cause higher rejection rates in production unless curing or mix adjustments compensate.
6.Conclusion
Mix design for paver blocks on automatic block machines is a calibration problem, not a recipe retrieval problem. The published ranges—cement 350–400 kg/m³, W/C 0.35–0.40, total moisture 6.5–7.0%—provide a starting envelope, but the operative variables are aggregate moisture variability, machine compaction capability, and the early-strength requirement imposed by immediate demolding. Engineers and buyers should treat any mix proportion as provisional until validated on the specific machine with the specific aggregates, and should prioritize moisture control instrumentation over mix formula optimization as the first intervention when block quality varies.
If you want to get more information about our products, you can click www.yxbrickequipment.com